A Beginner’s Guide to CNC Machining: From 3D Design to Finished Part
Turn a 3D model into a usable part: choose a machining method, prepare toolpaths, set up the machine, cut the material, and check the result.
CNC means computer numerical control. In machining, a computer guides a cutting tool to remove material from a blank, called stock. Your model describes the finished shape; you still decide how to hold it, reach its features, and cut it accurately.
The workflow is CAD model → CAM toolpaths → machine-specific G-code → setup and cutting → inspection. We’ll follow a small mounting plate through that process.
1. Choose a process that fits the part
| Process | What moves | Typical parts |
|---|---|---|
| Milling | A rotating cutter moves relative to held stock | Brackets, pockets, housings, molds |
| Routing | Similar to milling, often over a large bed | Wood panels, plastic plates, signs; aluminum on suitable machines |
| Turning on a lathe | Stock rotates against a cutting tool | Shafts, spacers, knobs, threaded round parts |
On a 3-axis mill or router, X and Y cover the table plane and Z controls height. 2.5D machining makes flat floors and walls at selected depths. 3D machining follows curved surfaces, changing depth along the cut. Both can use the same 3-axis machine. Extra rotary axes provide access to more sides; many parts simply need to be flipped and located again.
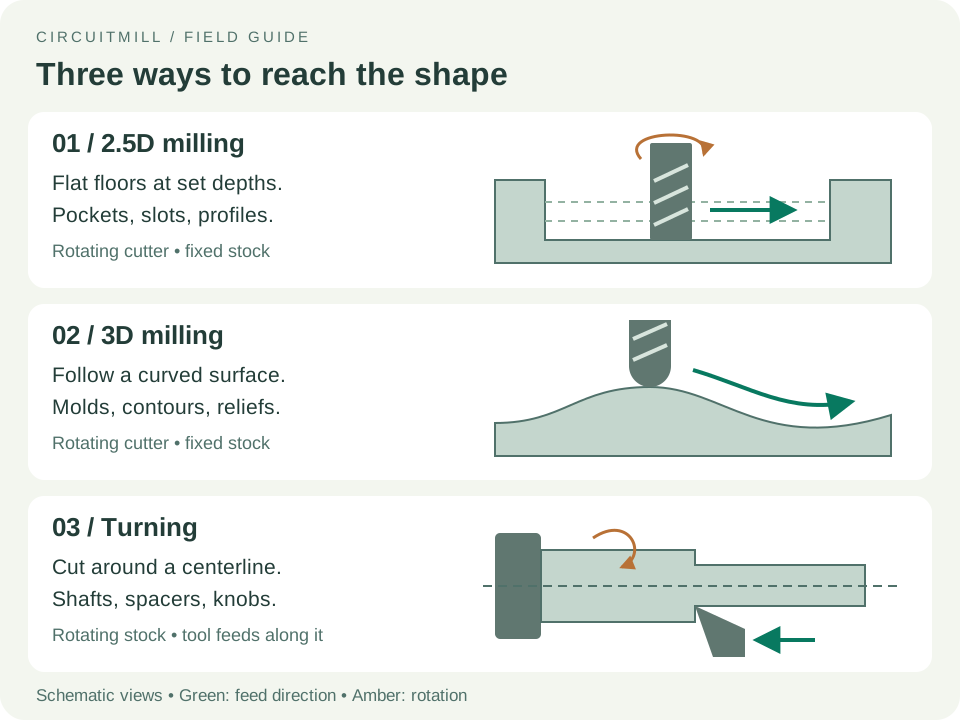
For a first project, choose a flat plate with a shallow pocket and through-holes. Machinable wax suits a practice cut; acetal suits many functional plastic parts; 6061 aluminum suits metal parts when the machine is capable. Choose material for the part’s load, temperature, and environment as well as the machine’s capabilities.
2. Make the model machinable
Start with a solid model in CAD (computer-aided design). Keep it native when CAD and CAM share an application, or export STEP for solid geometry. STL is a triangle mesh: use it only when your CAM workflow supports it, with enough resolution to preserve curves. Check units and overall dimensions after import.
- Leave room for a round cutter. Internal vertical corners retain a radius. A 6 mm cutter cannot make a corner smaller than 3 mm radius; a slightly larger design radius gives it room to turn. Use reliefs, often called dogbones, when a square mating piece must fit.
- Keep features reachable. Deep narrow pockets need long, flexible tools. Undercuts need another setup or special tooling.
- Provide something to grip. Leave extra stock for a vise, clamps, or tabs. Plan how the part stays held during the last cut.
- Specify what must fit. Add a drawing with material, critical dimensions, tolerances, hole locations, and threads. Tolerance is the permitted size variation; tighter requirements increase machining and inspection effort.
Our example is a 60 × 40 × 8 mm mounting plate, with a 30 × 20 mm pocket, 2 mm deep, internal corner radii of 4 mm, and four 4.5 mm through-holes for M4 clearance. Hole centers sit 7 mm from adjacent outside edges. These are example design dimensions, not cutting settings.
3. Match tools to features
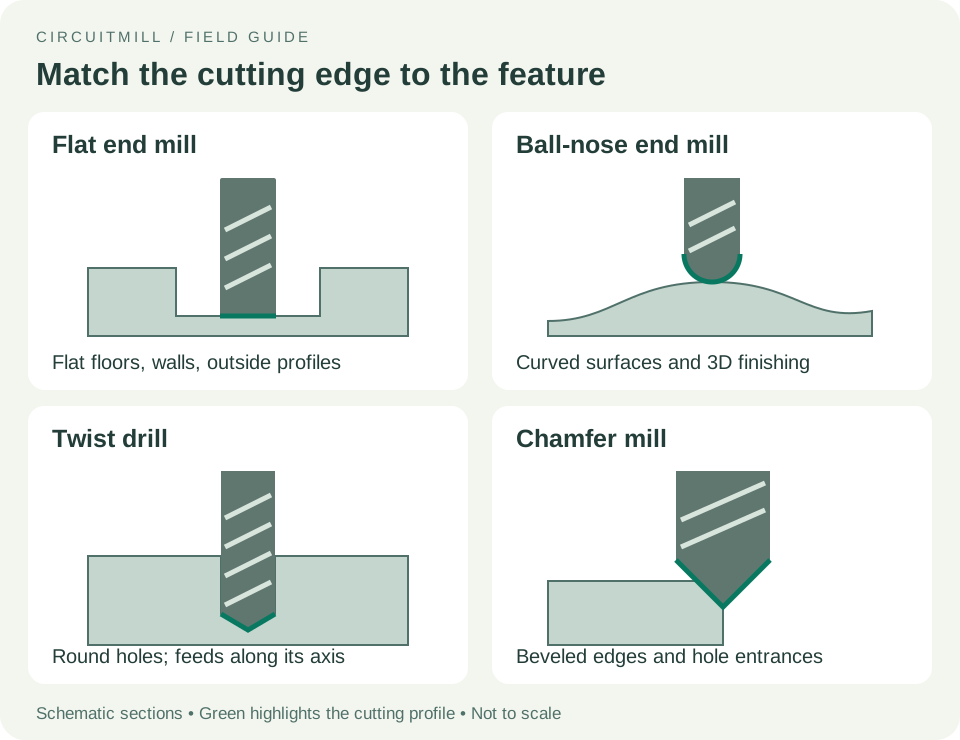
Use a flat end mill for the plate’s pocket and perimeter, a twist drill for its holes, and a chamfer mill or hand deburring tool to remove sharp edges. A ball-nose end mill is useful for sculpted surfaces. A face mill can flatten broad surfaces when the spindle and machine support it.
For precision holes, drilling may be followed by boring to correct diameter or reaming to finish an accurately prepared hole. A tap or thread mill produces internal threads; a clearance hole has no thread.
Choose tools rated for the material, with enough cutting length for the feature. Fewer flutes—the grooves that carry chips away—often provide more chip space for plastics and aluminum; follow the manufacturer’s application guidance.
What is a collet?
A collet is a slotted sleeve inside the spindle or tool holder that grips the cutter’s shank, its smooth cylindrical section. Tightening the collet nut squeezes the sleeve around the shank, holding the tool securely and centered as it rotates.
Match the collet’s series to the holder and its rated gripping range to the shank diameter. For example, a cutter with a 1 mm cutting tip may have a 3.175 mm (⅛-inch) shank: size the collet for that shank. Grip the smooth shank, keep the mating surfaces clean, and follow the holder’s insertion-depth and tightening instructions. Keep tool overhang—the length protruding from the holder—as short as the job allows to reduce flex and vibration.
4. Build the CAM setup and toolpaths
CAM—computer-aided manufacturing—calculates the cutter’s route. In a CAM package such as Autodesk Fusion, define the actual stock, model, fixtures, tools, and work coordinate system (WCS). Choose an accessible origin you can locate physically, such as a stock corner or a hole center, with positive Z pointing away from the top face. Set travel heights to clear clamps and stock. Autodesk’s setup reference explains these setup elements.
Common operations do different jobs:
| Operation | What it accomplishes |
|---|---|
| Facing | Flattens a surface and establishes a reference |
| Pocketing / adaptive clearing | Removes enclosed material; adaptive paths manage cutter engagement |
| Contouring / profiling | Follows a wall or outside boundary |
| Drilling | Creates holes; peck cycles retract between cuts when chip evacuation requires it |
| 3D finishing | Sweeps across curved surfaces, often with a ball nose |
| Chamfering | Bevels edges and hole entrances |
Roughing removes most material while leaving a small allowance. Finishing removes that allowance to reach size and improve the surface. Use a ramp or helical entry when appropriate; straight plunging requires a suitable cutter and cutting data. A smaller cutter can rest-machine corners the larger tool could not reach. Autodesk’s machining overview describes roughing and finishing strategies.
In climb milling, the workpiece feeds relative to the cutter in the same direction as the cutting edge’s motion at contact; conventional milling reverses that relationship. Climb milling is common on rigid CNC machines with controlled backlash, but use the strategy supported by your machine and workholding.
Set speed, feed, and depth together
- Spindle speed (RPM): how fast the cutter rotates.
- Feed rate: how fast it advances, usually mm/min or inches/min.
- Stepdown: depth added per layer. Stepover: sideways spacing or engagement between passes.
- Chip load: feed per cutting tooth; too little can rub and overheat, too much can overload the tool.
For a typical end mill, feed rate = RPM × flute count × chip load. For illustration, 10,000 RPM × 2 flutes × 0.03 mm/tooth = 600 mm/min. This demonstrates the arithmetic, not a recipe for your machine. Start with the tool maker’s data for your material, diameter, and operation, then account for rigidity, engagement, and chip removal. Sandvik’s milling formulas define these relationships.
5. Plan workholding before cutting
A vise suits blocks; clamps on a sacrificial spoilboard suit plates and sheet stock. Soft jaws or locating pins help repeat a position after flipping. Clamping should resist cutting forces without bending the part.
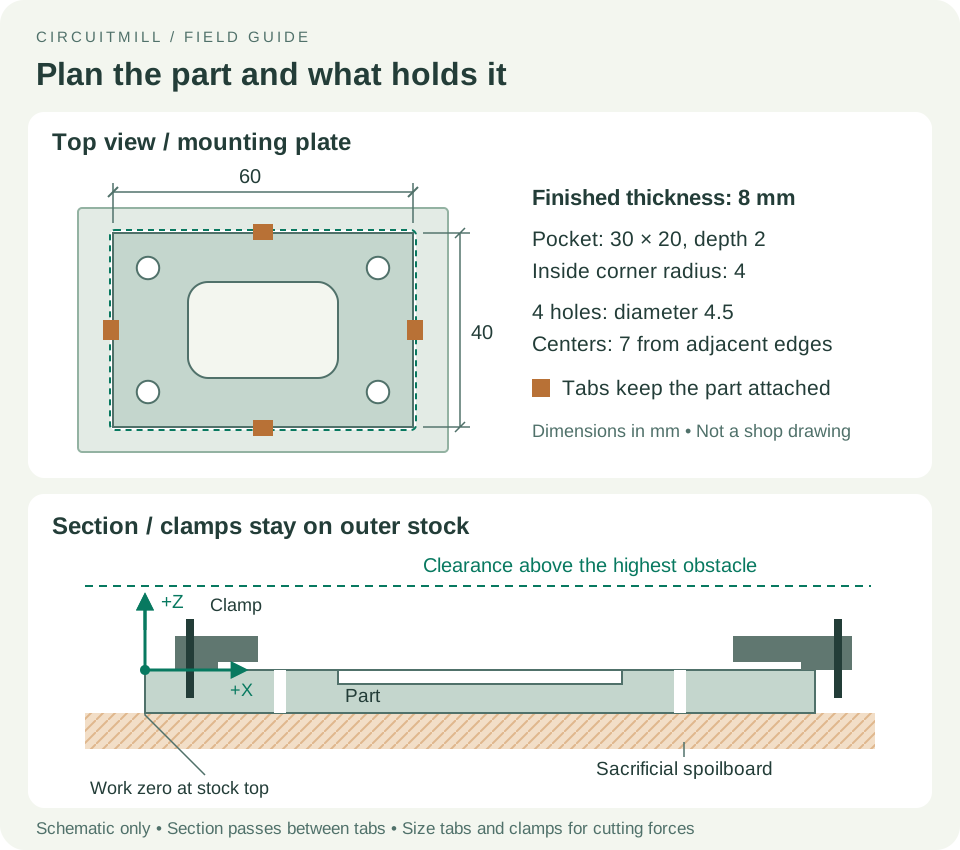
For the example plate, one approach is a larger blank with an already flat, verified 8 mm thickness. Clamp the surrounding material to a spoilboard and keep clamps outside every tool and holder path. Drill and pocket while the stock is intact; cut the perimeter last, leaving tabs. Allow drill-tip and profile breakthrough into the spoilboard without reaching the machine table.
If thickness or underside finish needs machining, start thicker and plan a second setup. Flip onto a known reference, secure and re-locate the part, then face to final thickness. Each setup needs its own verified origin.
6. Simulate, then generate the machine program
Simulate all operations in order, including stock removal. Check remaining material, gouges, tool and holder collisions, fixture clearance, breakthrough, and machine travel where supported. Simulation only knows the geometry and machine details you supplied.
Use a post processor matched to the machine and controller to generate G-code. A STEP file is not a machine program, and G-code is not universally interchangeable. Confirm units, work offset, tool changes, spindle commands, and retract behavior. For a manual tool-change machine, follow its supported workflow; this may mean separate programs per tool. Transfer the output using the controller’s supported method. Autodesk’s post-processing guide explains this conversion.
7. Set up and make the first cut
Follow your machine’s operating procedure and learn its stop controls before running a program. Wear eye protection, secure hair and loose clothing, keep guards closed, and use appropriate dust extraction or coolant for the material. Never wear gloves near rotating machinery or clear chips while it moves. Haas’s safety guidance covers core operating precautions.
- Home the machine, secure the stock, and install the correct tool in a clean, properly tightened holder.
- Locate the work origin with the machine’s supported probe or edge-finding method. Homing establishes machine coordinates; it does not locate your stock.
- Set and verify tool length / Z reference using the controller’s procedure. Recheck after every manual tool change. The physical work offset must match CAM. Haas’s part-setup guide distinguishes work and tool offsets.
- Prove out the program with controller graphics and the manufacturer’s dry-run or single-block procedure. Check initial moves and clearances with reduced rapid override where supported. If an approved air cut changes offsets, restore and verify them before cutting.
- Cut under supervision. Watch chip removal, vibration, and workholding. Stop for unexpected motion, squealing, chip buildup, or movement of the stock; diagnose before resuming.
For our plate: pocket roughing → pocket finishing → drill holes → profile with tabs → accessible edge chamfers. Add facing first if required, accounting for the material removed. Keep the part securely held throughout.
8. Finish, measure, and try the assembly
Once motion has stopped, remove the part, cut off tabs, and deburr edges and hole exits. Clean away chips. Measure overall size, thickness, pocket depth, and hole positions against the drawing; calipers suit general checks, while tighter requirements need appropriate micrometers, gauges, or other inspection tools.
Test the intended assembly: do screws pass freely, does the mating piece seat, and does the plate sit flat? A part is finished when it meets its dimensions and function, not just when the program ends.
| Problem | First things to check |
|---|---|
| Wrong size or position | Units, work origin, cutter diameter, remaining finish allowance |
| Chatter or rippled walls | Loose stock, excessive tool overhang, cutting engagement |
| Melted plastic or packed chips | Tool suitability, sharpness, chip evacuation, speed/feed balance |
| Poor hole fit | Burrs, drill runout, required boring or reaming operation |
Save the CAD, drawing, CAM setup, tool list, proven cutting settings, and final program together. Record measured results so the next part is repeatable.
For a PCB project, see our guide to PCB milling with CircuitMill. CircuitMill’s PCB workflow uses board fabrication data; a general 3D mechanical part needs a CAM workflow that supports its solid model and machining operations.